Daulatabad, Gurugram|ISO Certified
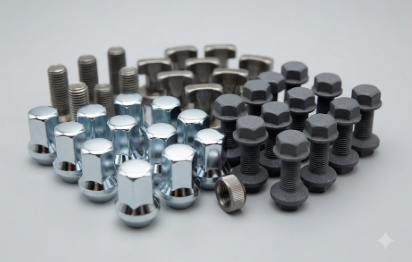
Some parts are more hole than steel — hollow pin, spacer tube, long sleeve with bore running most of length. We call these long-hole parts, one of more demanding things a cold forging shop can make.
FASTENER TECH produces long-hole components for automotive & industrial customers to drawings — Gurugram.
Hollow pins, spacer tubes & deep-bore sleeves — forged bore, not drilled. Concentric, work-hardened & material saving.
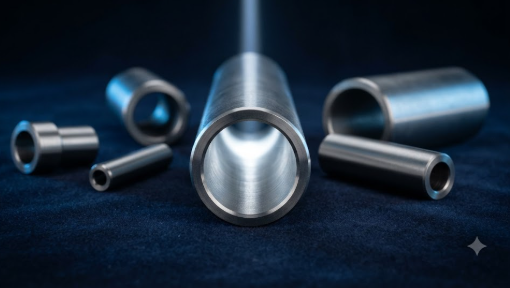
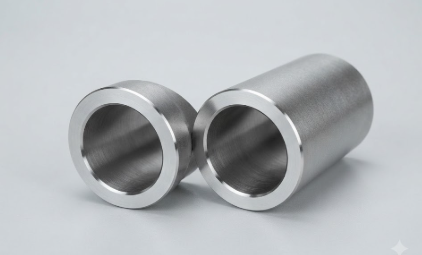
Any component where bore is deep compared with its diameter. Short bush with hole through is easy. Sleeve where hole is three, four or five times deeper than wide is different challenge.
If bore half cross-section, half steel leaves as swarf. Deep drilling slow & wanders.
But fixed sizes, costs more per kg than wire. Can't give flange/step/closed end without extra ops.
Solid slug sits in die. Punch driven into it, steel flows backwards around punch & forms wall. For deeper holes work shared across several stations.
Long punches slender — deflect or break if load not perfectly balanced. Slug must be cut to exact weight, since extra steel has nowhere to go. All comes down to tooling design & tool room discipline.
Length & concentricity checked vs drawing.
Yes — main advantage over tube. Formed in same sequence.
Through or blind hole — 4 to 14mm bore, OD 8-22mm, up to 60mm length. Hollow pins, spacer tubes & deep-bore sleeves.
Depends on diameter & material. Send drawing we'll give clear answer.
For most uses yes, generally more concentric. Very tight bores can be finished by machining.
Yes — that's main advantage over tube.
Often we can — we'll compare cost for you.
Share bore dia, OD, length, through/blind & monthly qty. Drawing ho to upload.